From concept to product
From prototyping to production, our production sites can handle all your manufacturing projects.
What thickness of metal can be fabricated?
The short answer
Sheet metal fabrication runs from roughly 0.3 mm to 25 mm, and most production parts sit between 0.5 mm and 6 mm. The ceiling belongs to the process, not the shop: shearing and punching stop near 6 mm, press brake bending at about 12 mm, fiber laser cutting reaches 25 mm in mild steel, and plasma or waterjet take over above that. Cut edges normally hold plus or minus 0.1 mm.
Where sheet ends and plate begins
There is no single number, because the limit is not a property of the metal. It is a property of the machine that has to hold it, cut it and bend it. The practical dividing line most shops work to is about 6 mm. Below that, coil handling, turret punches and standard press brake tooling all behave normally, and the part nests comfortably on a 1,220 by 2,440 mm sheet. Above it, handling weight, cutting speed and bending tonnage start to change the economics faster than they change the geometry.
That is why a straight answer is a set of ranges rather than one figure, and why the thickness on a drawing usually selects the process before any other feature does.
Thickness range, process by process
The bands below are production ranges, not laboratory maxima. Each process can be pushed past its band, but the cost per part stops being sensible, either because cut speed collapses or because the secondary work needed afterwards removes the advantage.

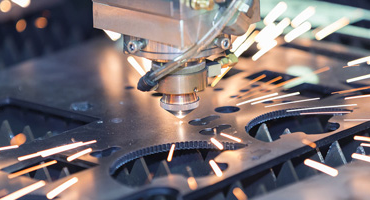
Three of those bands decide most quotes. Fiber laser cutting is the default between 0.5 mm and 20 mm because nothing else combines that tolerance with that speed - a 6 kW source cuts 16 gauge mild steel at around 8,000 mm per minute. Press brake bending is usually the real constraint, not cutting: a 200 tonne brake handles roughly 6 mm across a one metre bend, 500 tonnes reaches about 10 mm, and 16 mm needs a 1,000 tonne machine. Waterjet is the escape route for anything above 25 mm or anything that must not see heat at all.
The band decides the process and the tolerance
Thickness does not only pick the machine. It also sets how much tolerance is realistic, and how much design care the feature needs. The table below is the version we use at quoting time.

Four checks before you commit a thickness
Each of these can override the one before it, which is why the order matters. Cutting is checked first because it is the cheapest thing to change.

| If the drawing says | Check first | Because |
|---|---|---|
| 0.1 to 0.5 mm | Fixtures and nesting | Thin stock distorts in handling, not in cutting |
| 0.5 to 3.0 mm | Hole-to-bend distance | Holes need 2.5 times the thickness clear of the bend |
| 3.0 to 6.0 mm | Press brake tonnage | Bending force rises with the square of the thickness |
| 6.0 to 12.0 mm | Die width and bend radius | Wide V-die needed, inside radius at least one thickness |
| 12.0 to 25.0 mm | Cutting method and edge taper | Laser speed drops; plasma leaves a bevel |
| 25 mm and up | Joining and handling | This is plate fabrication, not sheet metal work |
Where the thin end breaks down
- Minimum hole size follows the thickness. As a rule the smallest practical hole diameter is about one times the material thickness, and the minimum slot width about 0.8 times. Below that the cut needs extra passes, more heat and leaves dross on the underside.
- Handling becomes the process. Below about 0.5 mm the part bends under its own weight, so the cost sits in fixtures, magnetic handling and flat packing rather than in the machine.
- Welding has a floor too. Thin walls under roughly 0.8 mm are difficult to weld without burn-through, which pushes the design towards riveting, clinching or adhesive bonding.
Where the thick end breaks down
- Edge taper appears. Laser perpendicularity stays within about one degree up to 10 mm, while plasma typically leaves a two to five degree bevel that needs grinding before a weld.
- Bend radius grows with thickness. One times the thickness is the practical minimum for mild steel, about 1.5 times for stainless, and around 2 times for 6061-T6 aluminium. Tight radii on thick stock crack on the outside of the bend.
- Tolerance loosens as thickness rises. The plus or minus 0.1 mm that is routine at 2 mm becomes plus or minus 1.5 mm at 30 mm, so features that must stay precise are usually machined after forming rather than formed.
- Long flanges stretch. Flanges grow by roughly 0.5 to 1.5 percent during forming, which shows up as a shift in hole position on long parts unless the flat pattern allows for it.
Do not specify the tightest tolerance on the sheet. Tolerance and thickness are independent decisions. General tolerances to a standard block such as ISO 2768 class m cover undimensioned features, and calling out plus or minus 0.05 mm on a feature nothing depends on adds inspection cost without adding function.
Thickness review at SOMI Custom Parts
We cut with fiber laser, plasma and waterjet, form on press brakes from 0.5 mm to 12 mm, run progressive dies from 0.3 mm to 6 mm, and weld from 0.8 mm upwards, so the thickness on your drawing is matched to a route rather than forced onto one machine. Send the drawing with an annual quantity and we will come back with the process, the flat pattern and the tolerance each feature can actually hold: see sheet metal fabrication, laser cutting, or open a project through our inquiry form.
Scope and sources. Thickness bands, tonnage figures and tolerance ranges above are typical published values for commercial sheet metal work in 2026 and were cross-checked against public process references including process and tolerance tables for sheet metal fabrication and shop capability data for fiber laser, plasma and waterjet cutting. Real limits move with material grade, machine power, tooling and part geometry, so treat these as planning ranges rather than quotations. Undimensioned features follow the general tolerance block on the drawing, for example ISO 2768 class m.
Are you looking for a reliable manufacturer of down home textile products?
We can quickly provide customers with market analysis, technical support and customized services.From concept to product
From prototyping to production, our production sites can handle all your manufacturing projects.
subscription