From concept to product
From prototyping to production, our production sites can handle all your manufacturing projects.
Metal Stamping
Home / Metal Stamping
SOMI Capability
SOMI Metal Stamping Capability
At SOMI, we specialize in high-precision custom metal stamping services designed to meet the diverse needs of various industries. As a leading custom metal stamping manufacturer, our state-of-the-art technology and experienced team enable us to deliver top-quality stamped components with exceptional accuracy and efficiency. We are committed to innovation and offer a wide range of metal stamping manufacturing processes, from prototyping to large-scale production. Our capabilities include intricate designs, custom tooling, and rapid turnaround times, ensuring that your project is completed on schedule and within budget.
Choose SOMI Custom Parts for reliable metal stamping that enhances your products' performance and durability.
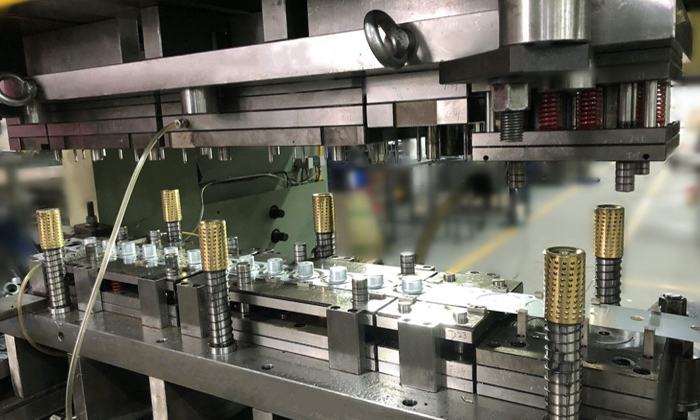
Metal Progressive Stamping
First, strip metal is feds through a progressive stamping press. The strip unrolls steadily from a coil and into the die press, where each station in the tool then performs a different cut, punch, or bend. The actions of each successive station add onto the work of the previous stations, resulting in a completed part.
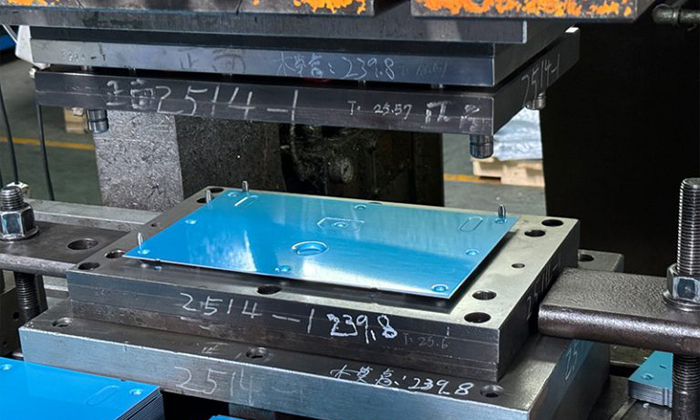
Metal Single-Stage Stamping Process
Single stage tooling (also referred to as manual dies) is a simpler process that relies on one stage, rather than multiple stages, to shape flat sheet metal (in coil form) to its predetermined specifications. During this tooling process, which also employs punching, blanking, embossing, bending, forming, drawing, flanging, coining, and more, a part is either loaded by hand (manual dies) or loaded by machine tending robots (transfer dies) onto a die’s surface.
Metal Stamping
Show Custom Metal Stamping Parts Machined by SOMI
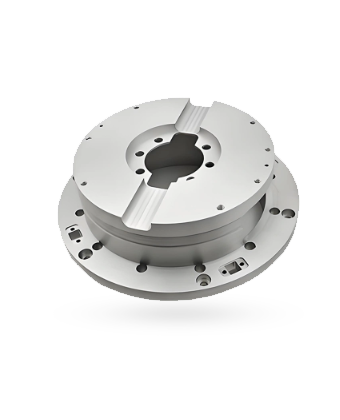
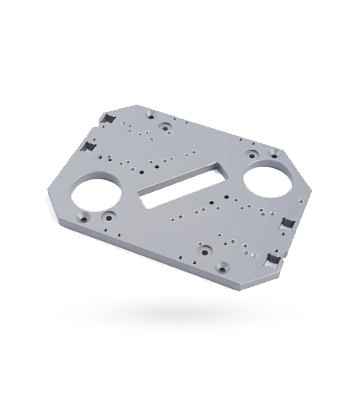
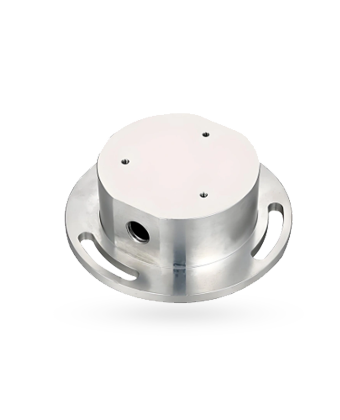
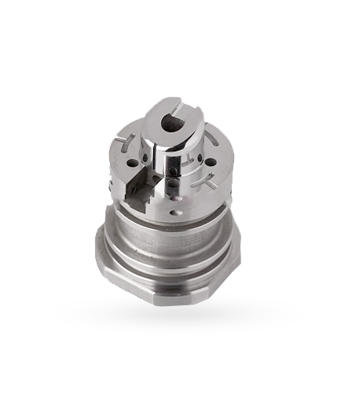
Metal Stamping
Metal Stamping Materials
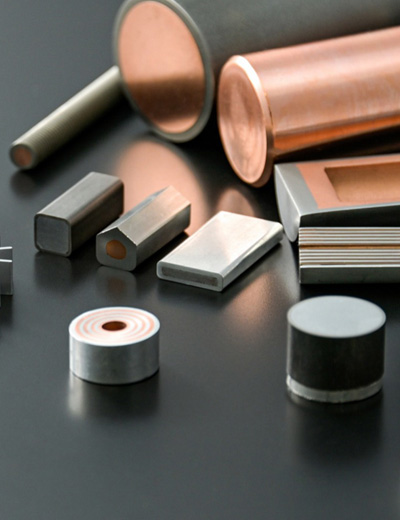
SOMI is committed to providing high-quality metal stamping services, supporting the processing of various metal materials to meet the diverse needs of different industries and applications. Below is an introduction to the common materials used in SOMI's metal stamping services and their characteristics: Metal Stamping Marerials List

- Aluminum
Aluminum has a good strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. It is a highly malleable metal, making it easy to machining, can be anodized.
Type:1050,1060,2011,2024,5052,5051, 6061, 6063, 7075,7050

- Brass
Aluminum has a good strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. It is a highly malleable metal, making it easy to machining, can be anodized.
Type:1050,1060,2011,2024,5052,5051, 6061, 6063, 7075,7050

- Stainless steel
Aluminum has a good strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. It is a highly malleable metal, making it easy to machining, can be anodized.
Type:1050,1060,2011,2024,5052,5051, 6061, 6063, 7075,7050

- Copper
Aluminum has a good strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. It is a highly malleable metal, making it easy to machining, can be anodized.
Type:1050,1060,2011,2024,5052,5051, 6061, 6063, 7075,7050

- Mild Steel
Aluminum has a good strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. It is a highly malleable metal, making it easy to machining, can be anodized.
Type:1050,1060,2011,2024,5052,5051, 6061, 6063, 7075,7050

- Beryllium bronze
Aluminum has a good strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. It is a highly malleable metal, making it easy to machining, can be anodized.
Type:1050,1060,2011,2024,5052,5051, 6061, 6063, 7075,7050

- Alloy steel
Aluminum has a good strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. It is a highly malleable metal, making it easy to machining, can be anodized.
Type:1050,1060,2011,2024,5052,5051, 6061, 6063, 7075,7050

- Titanium
Aluminum has a good strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. It is a highly malleable metal, making it easy to machining, can be anodized.
Type:1050,1060,2011,2024,5052,5051, 6061, 6063, 7075,7050

- Tool steel
Aluminum has a good strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. It is a highly malleable metal, making it easy to machining, can be anodized.
Type:1050,1060,2011,2024,5052,5051, 6061, 6063, 7075,7050
Metal Stamping
Metal Stamping Surface Finishes
SOMI offers a diverse range of surface finishes, each tailored to meet the specific needs of your projects. Here’s a closer look at some of the options.
As-machined
The standard finish of our parts, the "machined" finish, has a surface roughness of 3.2 μm (126 μin), which removes sharp edges and cleanly removes burrs from the part.
Machining Texture:There are slight scratches on the visible surface.
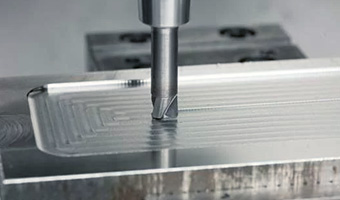
Smooth machining
A finishing CNC machining operation can be applied to the part to reduce its surface roughness. The standard smoothing surface roughness is Ra 1.6 μm (64 μin). Light surface scratches are visible.
Machining Texture:Visible, light surface scratches.
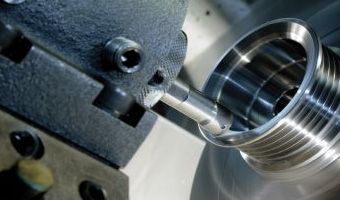
Fine machining
Refers to the process of precision treatment of raw materials or semi-finished products. The standard smoothing surface roughness is Ra 0.8 μm (32 μin).
Machining Texture:Slightly visible.
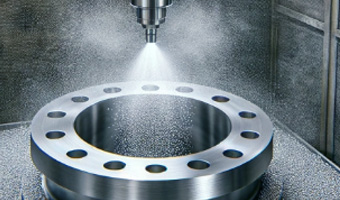
Bead blasting
Bead blasting refers to the use of round spherical media that, when impacted against the surface of a part, will leave a more uniform finish caused by the sphere “dimpling” the surface.
Machining Texture:Frosted grain.
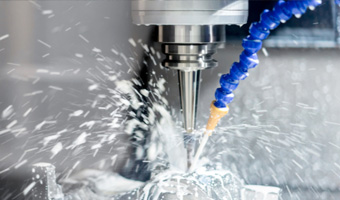
Brushing
Brushing is a surface treatment process that uses abrasive belts to draw traces on the surface of a material, usually for aesthetic purposes.
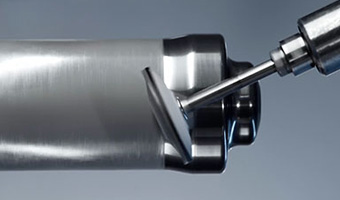
Polishing
From Ra 0.8 to Ra0.1, the polishing process uses abrasive materials to rub the surface of the part, making the surface of the part more shiny, depending on your requirements.
Machining Texture:Smooth, glossy finish
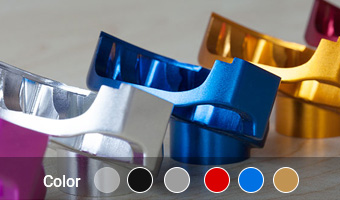
Anodizing
Aluminum and its alloy in the corresponding electrolyte and specific process conditions, due to the action of external current, the process of forming an oxide film on the aluminum product.
Machining Texture:Smooth, matte finish.
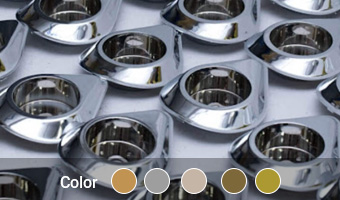
Electroplating
Electroplated coating preserves the surface of parts and resists rusts and other defects from causing decay by applying electric currents to reduce metal cations.
Machining Texture:Smooth, glossy finish.
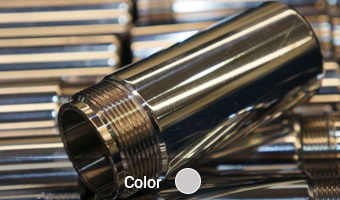
Electroless nickel plating
Electroless nickel plating is a process that deposits an alloy of nickel-phosphorus onto the surface of a metal. This process is chemical only, so does not involve the use of electricity.
Machining Texture:Reduced but visible.
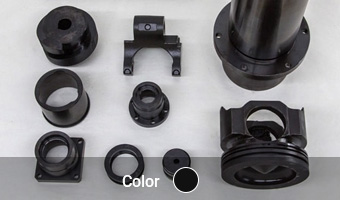
Black oxide
Black oxide is a conversion coating similar to Alodine that is used for steel and stainless steel. It is used mainly for appearance and for mild corrosion resistance..
Machining Texture:Smooth, matte.
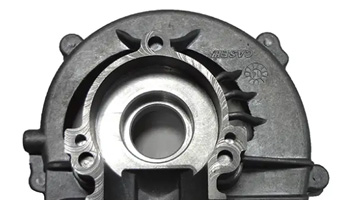
Powder coating
Using corona discharge, we make the powder coating adsorbed to the part, creating a more wear-resistant layer with a typical thickness ranging from 50 μm up to 150 μm.
Machining Texture:Glossy.
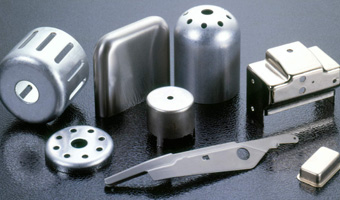
Chromate conversion coating
Chromate conversion coating is a type of conversion coating, used on aluminum as a corrosion inhibitor, as a primer for paint due to increased adherence or to preserve electrical conductivity.
Machining Texture:Visible.
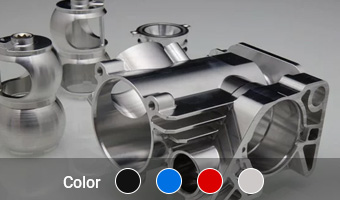
Electrophoresis
In the solution under the action of direct current electric field, the charged resin moves to the opposite electrode phenomenon. Strong corrosion resistance, can be on different colors.
Machining Texture:Visible.
As-machined
The standard finish of our parts, the "machined" finish, has a surface roughness of 3.2 μm (126 μin), which removes sharp edges and cleanly removes burrs from the part.
Machining Texture:There are slight scratches on the visible surface.
Smooth machining
A finishing CNC machining operation can be applied to the part to reduce its surface roughness. The standard smoothing surface roughness is Ra 1.6 μm (64 μin). Light surface scratches are visible.
Machining Texture:Visible, light surface scratches.
Fine machining
Refers to the process of precision treatment of raw materials or semi-finished products. The standard smoothing surface roughness is Ra 0.8 μm (32 μin).
Machining Texture:Slightly visible.
Bead blasting
Bead blasting refers to the use of round spherical media that, when impacted against the surface of a part, will leave a more uniform finish caused by the sphere “dimpling” the surface.
Machining Texture:Frosted grain.
Brushing
Brushing is a surface treatment process that uses abrasive belts to draw traces on the surface of a material, usually for aesthetic purposes.
Polishing
From Ra 0.8 to Ra0.1, the polishing process uses abrasive materials to rub the surface of the part, making the surface of the part more shiny, depending on your requirements.
Machining Texture:Smooth, glossy finish
Anodizing
Aluminum and its alloy in the corresponding electrolyte and specific process conditions, due to the action of external current, the process of forming an oxide film on the aluminum product.
Machining Texture:Smooth, matte finish.
Electroplating
Electroplated coating preserves the surface of parts and resists rusts and other defects from causing decay by applying electric currents to reduce metal cations.
Machining Texture:Smooth, glossy finish.
Electroless nickel plating
Electroless nickel plating is a process that deposits an alloy of nickel-phosphorus onto the surface of a metal. This process is chemical only, so does not involve the use of electricity.
Machining Texture:Reduced but visible.
Black oxide
Black oxide is a conversion coating similar to Alodine that is used for steel and stainless steel. It is used mainly for appearance and for mild corrosion resistance..
Machining Texture:Smooth, matte.
Powder coating
Using corona discharge, we make the powder coating adsorbed to the part, creating a more wear-resistant layer with a typical thickness ranging from 50 μm up to 150 μm.
Machining Texture:Glossy.
Chromate conversion coating
Chromate conversion coating is a type of conversion coating, used on aluminum as a corrosion inhibitor, as a primer for paint due to increased adherence or to preserve electrical conductivity.
Machining Texture:Visible.
Electrophoresis
In the solution under the action of direct current electric field, the charged resin moves to the opposite electrode phenomenon. Strong corrosion resistance, can be on different colors.
Machining Texture:Visible.
Industry
Application Areas of Metal Stamping
Our facilities are equipped with the latest in high-precision Metal Stamping equipment, capable of executing complex designs with exacting tolerances. From prototyping to full-scale production, It's comprehensive machining capabilities cater to a diverse range of industries, including aerospace, automotive, medical, and more.
Consumer Electronics
Our manufactured electronic components consistently meet the tight tolerances required in this ever-evolving industry.
Learn More
Aerospace & Aviation
Our manufactured electronic components consistently meet the tight tolerances required in this ever-evolving industry.
Learn More
Automotive
Our manufactured electronic components consistently meet the tight tolerances required in this ever-evolving industry.
Learn More
Medical
Our manufactured electronic components consistently meet the tight tolerances required in this ever-evolving industry.
Learn More
Robotics & Automation
Our manufactured electronic components consistently meet the tight tolerances required in this ever-evolving industry.
Learn More
Industrial Machinery Parts
Our manufactured electronic components consistently meet the tight tolerances required in this ever-evolving industry.
Learn MoreTest Inspection
Quality Assurance at the Heart of Our Operations
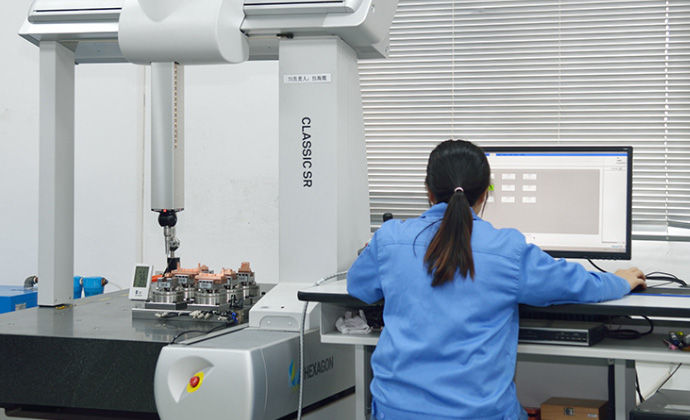
Quality is not just a buzzword at SOMI,it's the foundation upon which we build our reputation Our rigorous quality assurance process encompasses every stage of production, from initial design to final inspection. We employ advanced measurement and testing equipment to verify that each part meets our stringent standards and, more importantly, your expectations. This unwavering dedication to quality ensures that SOMI's Metal Stamping services are a step above the rest.
Get a Quote
Contact us Today for Your Metal Stamping Requirements
Ready to elevate your manufacturing with the precision and quality of SOMI's Metal Stamping services? Contact us today to discuss your project and discover how we can help you achieve unparalleled results. With SOMI, you're not just choosing a service provider, you're choosing a partner dedicated to your success.
We are committed to providing full-process services from prototyping to mass production. We provide rapid prototyping services to ensure that your design can be realized accurately and efficiently.
We hope to discuss potential cooperation opportunities with you and ask you to provide quotation information for your project. Looking forward to your reply and working with you to promote the success of your project!
- *Name
- *Phone
- *Title
- *Content
FAQ
Frequently Asked Questions
If you have any further questions, please contact us. We look forward to working with you.
- What is the difference between single-die and progressive-die stamping?
The short answer
A single-stage die performs one operation per press stroke - blank, pierce, or form - and the part has to be moved to another die for every additional feature. A progressive die puts 4 to 30 stations into one die set: strip feeds continuously, each station adds one or more features, and a finished part is sheared off at the last station on every stroke, up to 1,500 strokes per minute. As a working rule: stay with single-stage tooling below roughly 10,000 pieces per year or while the design is still changing, and move to a progressive die once annual volume passes about 50,000 pieces.
How the two tooling types work
Both approaches use the same press technology. The difference is how much of the part's geometry is consolidated into one tool, and how many times the part has to be located before it is finished.
Single-stage die
One operation per stroke from one die. The workpiece is transferred manually or robotically between independent presses or die stations until all features are complete.
Progressive die
One die set containing every operation, in sequence, with automatic coil feed. The strip is the transport system: the part is never released until the final cut-off.

Single-stage tooling moves the part between dies. A progressive die holds every station in one set. A third option sits between them. A compound die completes two or three operations at the same station in a single stroke, which is why it holds hole-to-edge alignment better than staged single dies on flat parts. Tooling typically lands between the two extremes at USD 3,000 - 10,000.
What "progressive" actually means, station by station
The part is carried on a carrier strip, kept at least twice the material thickness wide (commonly 3 - 15 mm) with pilot holes that register the strip into the die at every stroke. Because the strip position is fixed by the pilots, the positional relationship between features is set by the tooling rather than by how carefully an operator re-loads the part. Feed pitch accuracy of about ±0.01 mm to ±0.05 mm is what makes multi-feature parts repeatable.

A typical five-station sequence: pierce pilots, blank the outline, pierce holes, form ribs, cut off. The practical test we use on the shop floor is simple: how many times does the part get located before it is finished? One location per die, many times, produces tolerance stack-up. One location held to the last station produces a consistent part.
Side-by-side comparison
Factor Single-stage die Compound die Progressive die Operations per stroke 1 2 - 3, same station Multiple, across 4 - 30 stations Tooling cost USD 1,000 - 5,000 USD 3,000 - 10,000 USD 10,000 - 250,000+ Die lead time 2 - 4 weeks 4 - 6 weeks 8 - 20 weeks Practical volume 100 - 10,000 pcs 1,000 - 50,000 pcs 50,000+ pcs per year Feature tolerance Around ±0.1 mm, stack-up from re-location Around ±0.05 mm ±0.02 - 0.025 mm repeatable Output Operator or transfer paced Moderate Up to 1,500 strokes per minute; 7 - 50 parts per minute above 6 mm thickness Direct labour High Moderate Very low, typically one operator per line Material utilisation Moderate Moderate 75 - 90% of coil weight with a good strip layout Design change cost Low, fast die swaps Moderate USD 5,000 - 80,000 per modified station Best-fit parts Prototypes, simple flat parts, very large parts Flat parts needing tight hole-to-edge alignment Complex multi-feature parts at volume Cost, volume, and the breakeven point
The tooling invoice is not the whole number. Total cost has five parts: tooling, per-part processing, labour and handling, maintenance, and changeover downtime - and each die type behaves differently in each bucket. Progressive tooling also carries hidden costs that buyers miss, notably the carrier strip, which consumes material that a single-stage layout does not.

Progressive tooling starts higher and flattens quickly; single-stage tooling starts low and climbs with volume. - Tooling is normally recovered in 6 to 18 months at high-volume production rates.
- Replacing manual or CNC-based operations with progressive stamping has been reported to save USD 50,000 to 500,000 per part number per year at scale.
- Below roughly 50,000 - 100,000 pieces per year, the tooling investment usually does not pay back, and single-stage or compound tooling is the lower-cost route.
- Compared with multi-slide methods, progressive setups have been benchmarked at about 38% less setup time.
Precision, limits, and when not to choose a progressive die
Progressive dies repeat to about ±0.025 mm (±0.001 in) across long runs, which is why they dominate electrical terminals, connectors, and thin automotive brackets. The limits are just as specific:
- Coil width is bounded, roughly 5 - 500 mm, and finished parts commonly 5 - 300 mm. Larger structural parts fall back to single-stage or transfer stamping.
- Material thickness is practical up to about 6 mm; heavier stock needs dedicated presses that run at 7 - 50 parts per minute.
- Deep draws beyond roughly 0.5:1 depth-to-diameter usually need transfer tooling or a dedicated draw press.
- The design must be close to frozen. Every station change costs USD 5,000 - 80,000 plus lost production time.
Watch the maintenance schedule. A worn punch at station six can quietly produce thousands of out-of-tolerance parts before anyone notices. In-process dimensional sampling during long runs is what catches it, not final inspection.
Choosing in five questions
- What is the annual volume? Under 10,000 pieces, single-stage tooling wins. Over 50,000, progressive tooling usually wins. The 10,000 - 50,000 band is a compound-die conversation.
- How many features must align to each other? More than two or three pierced or formed features held in relationship points to a progressive die.
- Is the design frozen? If prints are still moving, a progressive die locks in change costs of USD 5,000 - 80,000 per station. Stage the tooling instead.
- Does the part fit the coil? Part size, material thickness, and coil width decide whether a progressive die is physically possible.
- What is the real landed cost? Compare tooling plus per-part plus labour plus maintenance plus changeover, not the tooling quote alone.
Stamping support at SOMI Custom Parts
We build single-stage, compound, and progressive tooling from 0.2 mm to 6 mm stock in carbon steel, 301/304/316 stainless, 5052 and 6061 aluminium, copper, and brass. Tooling design, strip layout, first-article dimensional reports, and in-process sampling sit in the same team that runs your press, so what gets quoted is what gets built.
Send us a drawing and an annual quantity and we will come back with the die type, station count, strip layout, and landed cost for both routes: progressive and single-stage metal stamping, sheet metal fabrication, or start a project through our inquiry form.
Scope and sources. Tooling cost ranges, press speeds, tolerance bands, and volume thresholds above are typical values published for commercial sheet-metal stamping in 2026 and were cross-checked against Xometry's progressive die stamping reference. Real numbers move with part geometry, material, press selection, and strip layout, so treat these as planning ranges rather than quotes. Feature tolerances are stated where called out; undimensioned features follow the general tolerance block on the drawing, for example ISO 2768 class m for sheet-metal parts.
Explore More
SOMI Manufacturing Capabilities


From concept to product
From prototyping to production, our production sites can handle all your manufacturing projects.
subscription