From concept to product
From prototyping to production, our production sites can handle all your manufacturing projects.
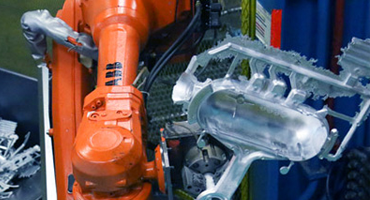
Why are aluminum alloys popular for die casting?
The short answer
Aluminium alloys account for over 70 percent of die-cast parts because they combine a strength-to-weight ratio of 200 to 330 MPa at 2.7 g/cm3 with fast 20 to 90 second cycles, thermal conductivity of 92 to 170 W/m.K, as-cast tolerances of plus or minus 0.1 to 0.25 mm and complete recyclability. No competing casting metal delivers all five at the same cost.
Six reasons aluminium dominates
Aluminium is popular because it is never the best at any single property but is competitive on all of them at once. That balance is what a production decision actually needs.
- Strength at a third of the weight of steel. Aluminium is about 2.7 grams per cubic centimetre against 7.8 for steel, so a die-cast aluminium bracket carries a comparable structural load at roughly a third of the mass. In vehicles and hand-held products that weight saving is the whole business case.
- Near-net shape with integrated features. Ribs, bosses, mounting pads, undercuts and internal channels are formed in a single shot that would otherwise need several pressings plus welding and assembly. Net-shape output typically removes 60 to 80 percent of the material waste of machining from billet and cuts total component cost by 20 to 40 percent against fabricated alternatives.
- Thermal conductivity that does structural work. At 92 to 170 W/m.K, an aluminium housing doubles as a heat sink, which is why motor housings, inverter cases, LED drivers and power modules are cast rather than fabricated.
- High production rates. Cycle times of 20 to 90 seconds per shot support outputs of tens of thousands to hundreds of thousands of parts per cavity per year once tooling exists.
- Repeatable as-cast tolerances. Standard as-cast linear tolerance is around plus or minus 0.1 mm for features under 25 mm, widening to plus or minus 0.25 mm over 250 mm, which removes most secondary machining on non-critical features.
- Recyclability and a mature supply base. Aluminium is recyclable without losing mechanical properties and runner and overflow metal goes straight back into the melt. Modern foundries run substantial recycled content, and alloy supply and machine capacity are available almost anywhere.
The numbers behind the claim
The following table is the version we use in a quotation review, because these are the figures a purchasing team can test against a competing process.
| Metric | Typical value | Why it matters commercially |
|---|---|---|
| Density | 2.7 g/cm3 | Structural parts at a third of steel weight |
| Tensile strength as cast | 200 - 330 MPa | Covers brackets, housings and frames |
| Thermal conductivity | 92 - 170 W/m.K | Removes a separate heat-sink component |
| Injection pressure | 70 - 150 MPa | Fills 1 to 4 mm walls reliably |
| Cycle time | 20 - 90 seconds | High throughput per cavity |
| As-cast tolerance | plus or minus 0.1 to 0.25 mm | Less secondary machining |
| Machined tolerance | plus or minus 0.02 to 0.05 mm | Bores and sealing faces still work |
| Die life (H13 tooling) | 200,000 - 350,000 shots | Tooling amortises over a long program |
| Tooling lead time | 5 - 8 weeks | Bridge tooling can cut this to 3 - 5 weeks |
| Break-even against machining | about 3,000 - 5,000 parts | Where the tooling investment pays back |
Aluminium against zinc, magnesium and steel
Comparing the same part across materials is the quickest way to see why aluminium is the default. Zinc wins on precision, die life and cycle time but loses on weight. Magnesium wins on weight but loses on cost and corrosion. Steel wins on strength but cannot be die cast at all, so it competes as a pressing or a weldment.

Thermal conductivity is the quiet advantage
Strength and weight get the attention, but conduction is the reason aluminium appears in so many electronics and motor applications. A die-cast aluminium housing can act as the heat path itself, so the design deletes a separate heat sink, its fixing hardware and the thermal interface between them. That is a component-count reduction, not just a material substitution, and it frequently decides a program before cost is discussed.

Inside aluminium: which alloy and when
Aluminium is a family, and the grade changes the answer more than most buyers expect. A380 and ADC12 are the general-purpose castability and cost choice for housings, brackets and gearbox covers. A383 is preferred where fill quality on thin walls decides the result. A360 trades a little castability for corrosion resistance and pressure tightness, which matters on anything that must not leak, such as a hydraulic body. A356 T6 is more ductile and heat treatable and is specified for structural and safety-related parts where elongation matters as much as strength. B390 with its high silicon content delivers wear resistance for pump and engine surfaces, at the price of accelerated die wear.
When aluminium is the wrong choice
- Aluminium loses strength above roughly 300 C. Sustained high-temperature service, such as a hot exhaust-side component, usually needs a different material or a different process.
- Very thin walls with short flow paths belong to zinc. Aluminium reaches about 1.2 mm only over a limited flow length. Claims of 0.8 mm on aluminium generally refer to a test coupon, not a production part.
- Thick sections are the hardest thing to cast, not the easiest. Above about 8 mm, solidification time rises steeply and the interior shrinks into porosity. Where mass is genuinely needed, core the section out and add ribs.
- Low volumes cannot carry the tooling. Under roughly 3,000 parts, machining from billet or sand casting is usually cheaper than amortising an aluminium die.
- Tight bores and sealing faces still need machining. The as-cast tolerance will not hold a bearing fit, so plan the secondary operation into the design and the price.
- Wrought alloys such as 6061 are not die-casting alloys. They hot-crack and stick, so the alloy must be chosen from the casting family.
Cost, break-even and what we need to quote
The economics are simple to describe and easy to get wrong. Tooling for aluminium runs from roughly USD 8,000 to USD 80,000 or more depending on size and cavity count, and a typical 0.8 kg casting lands between about USD 3 and USD 5 per part excluding tooling. The break-even against machining usually falls around 3,000 to 5,000 parts. Above that, per-part cost keeps falling as the tool amortises, which is why aluminium die casting is described as the lowest total cost of ownership among precision metal forming routes for annual volumes above roughly 10,000 units.

To quote properly we need the drawing or STEP file, the alloy if you have a preference, the annual volume and expected program life, the load case and the environment, and any surfaces that must remain as-cast. With those we will return DFM feedback on walls, draft and porosity risk alongside the price at two volumes, so the break-even is visible rather than asserted. We cast aluminium and zinc and machine the critical features in house, and the related processes are listed under aluminium die casting, surface finishing and metal stamping for the sheet-metal alternative.
Scope and sources. Property values, cycle times, tooling ranges and break-even points were compiled in 2026 from an overview of aluminium die casting benefits and cost drivers, a design guideline and cost model with NADCA tolerance grades, a die casting process guide covering tooling cost and cycle time and a comparison of aluminium, zinc and magnesium die-cast alloys. Tooling, unit price and die life depend heavily on part geometry, cavity count, alloy and program length, so the figures here are planning bands for budgeting rather than quotations. Confirm them against a DFM review and first-article inspection before committing to a program.
Are you looking for a reliable manufacturer of down home textile products?
We can quickly provide customers with market analysis, technical support and customized services.From concept to product
From prototyping to production, our production sites can handle all your manufacturing projects.
subscription