From concept to product
From prototyping to production, our production sites can handle all your manufacturing projects.
Home / All / Metal Stamping / What types of parts are most commonly produced by custom metal stamping services?
What types of parts are most commonly produced by custom metal stamping services?
The short answer
Custom stamping suits almost anything that can be cut or formed from flat sheet: automotive brackets, electrical terminals, EMI shield cans, washers and shims, heat-sink fins, appliance panels. The shared conditions are a sheet form, a thickness under about 6 mm, a simple 2D or formed shape, and volume above roughly 10,000 parts a year.
The one condition every stamped part shares
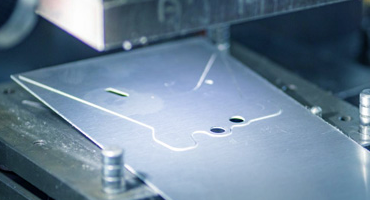
Stamping is not one process but a family of them, and every member starts from flat stock. Blanking cuts the outline, piercing makes the holes, bending folds along a line, and drawing pulls the sheet into a cup or channel. A progressive die chains those operations together and feeds coil from a reel, so a single press stroke can produce a finished part with a tab bent and a hole pierced in the same cycle. That is why the governing property of a stamped part is not its shape but its material form: if the part cannot be described as a flat development plus a set of bends, drawing is usually the wrong conversation.
The second consequence is consistency. Once a die is set, every stroke produces a geometrically identical part, with variation driven by die wear and coil thickness rather than by operator skill. Standard stamping holds around plus or minus 0.1 to 0.4 mm, precision progressive tooling reaches plus or minus 0.02 to 0.05 mm, and the whole point is that the same number holds at part one and part one million. That repeatability, not the per-part price, is what makes stamping the default for safety-critical brackets and connectors.
Six part families that make up most stamping work
Automotive is the largest consumer of stampings by a wide margin, and industry estimates put 60 to 70 percent of all automotive parts as stampable. That covers body panels and reinforcement plates in mild and high-strength low-alloy steel, plus the small parts nobody sees: motor mounts, seat tracks, fuel-tank straps, brake backing plates and heat shields. Thickness runs from 0.5 mm decorative trim to 6 mm structural brackets, and the parts are typically run on progressive or transfer dies at volumes from 100,000 to more than 2 million a year.
Electrical and electronic parts form the second family and the highest-volume one. Connector pins and sockets, terminals, relay and switch components, battery contacts, and the EMI and RFI shielding cans that sit over a radio or a motor driver are all stamped, usually from brass, phosphor bronze, tin-plated steel or stainless. These parts are thin, often 0.05 to 0.5 mm, and they demand edge quality rather than stiffness, with dimensional control often quoted at plus or minus 0.05 mm. A third family covers washers, shims, spacers and retaining rings in carbon steel, where the tolerance that matters is thickness consistency rather than profile. A fourth covers heat-sink fins and lids in aluminium, where formability and thermal contact matter more than strength. A fifth covers appliance and enclosure panels and brackets in cold-rolled and galvanised steel, where the visible surface is the deliverable. The sixth covers nameplates, tags and decorative trim, where the die is simple and the finish is the value.
| Part family | Typical parts | Material | Thickness | Annual volume |
|---|---|---|---|---|
| Automotive structural | Mounts, reinforcement plates, heat shields, seat tracks | Mild steel, HSLA steel | 0.5 to 6 mm | 100,000 to 2 million |
| Electrical contact | Terminals, connector pins, relay parts, lead frames | Brass, phosphor bronze, tin-plated copper | 0.05 to 0.5 mm | 500,000 to 50 million |
| EMI and battery | Shielding cans, battery tabs, contacts | Tin-plated steel, stainless | 0.15 to 0.8 mm | 100,000 to 5 million |
| Washers and shims | Flat, lock and spring washers, shims, spacers | Carbon steel, stainless | 0.1 to 3 mm | 100,000 to 10 million |
| Heat sink and fin | Fin packs, thermal lids, heat spreaders | Aluminium 1100, 3003 | 0.3 to 2 mm | 10,000 to 500,000 |
| Appliance and panel | Panels, brackets, handles, nameplates | Cold-rolled, galvanised steel | 0.4 to 2 mm | 50,000 to 1 million |

How to tell whether your part is a candidate
Four questions settle it, and they are worth answering before a die is quoted. First, can the part be developed from flat sheet, meaning is it a profile plus bends and possibly a shallow draw? A part with a deep pocket, an internal thread or a varying wall thickness is not a stamping candidate however high the volume. Second, is the thickness inside the working window? Stamping lives between roughly 0.1 and 6 mm; below that the coil is hard to feed and handle, and above it the press tonnage and the die cost rise steeply. Third, is the annual quantity high enough? The crossover against a no-tooling process usually sits between 5,000 and 10,000 parts a year for a simple part, so a programme below that number is usually better served by laser cutting, punching or machining. Fourth, is the tolerance requirement at or looser than about 0.1 mm? Anything tighter generally means coining or shaving in the die, a secondary operation, or a hybrid route that stamps the shape and machines the critical features.

The families, drawn by thickness
The thickness band is a useful cross-check because it correlates with both material and process. Contacts, pins and shield cans sit at the thin end, between 0.05 and 0.8 mm, and they are run on high-speed presses with fine blanking or precision progressive tooling to keep edges clean. Washers, shims, fins and appliance panels occupy the middle, roughly 0.1 to 3 mm, where the process is straightforward and the tooling is a conventional progressive die. Automotive structural brackets sit at the top, 0.5 to 6 mm, and they need heavier presses, stronger die steels and often a transfer rather than a progressive layout because the tonnage per station is higher.

Materials that behave well and materials that fight back
Four material groups cover most stamped parts. Cold-rolled low-carbon steel is the workhorse for brackets and panels because it forms predictably and welds easily. Galvanised and stainless grades are specified where corrosion resistance is required, with stainless 304 and 316 common in food equipment and medical housings; stainless is also the material that wears a die fastest, so it usually means a harder die steel and a shorter service interval. Aluminium alloys 1100 and 3003 are chosen for formability and 6061 where higher strength is needed after forming. Copper, brass and phosphor bronze are chosen for conductivity, and they are the classic connector materials; copper alloys work-harden during forming and may need an intermediate anneal in a deep draw. Where a spring property is required, beryllium copper or a spring steel such as 301 is specified, and the die then has to control springback rather than simply shape the part.
Where stamping stops being the right answer
Five cases should be routed elsewhere. A part with an internal thread or a threaded boss is not a stamping; the thread is either tapped in a secondary operation or the part belongs to machining or casting. A part that needs a varying wall thickness, a deep pocket or a true 3D contour cannot be developed from sheet and belongs to CNC or casting. A part inside a handful of hundreds of units a year cannot carry a die and should be laser cut, punched on a turret or machined. A part whose critical tolerance is tighter than about 0.05 mm usually needs coining, shaving or a post-stamping machining step. And a design that is still moving should not be committed to a die at all, because die modification is the most expensive form of engineering change there is.
Two limits close the subject. Every volume and thickness figure here is a planning range for quotation discussion, not a specification, and the real crossover for any part depends on die cost, material yield and the per-part saving. And the stamping family is not limited to these six; food container lids, construction ties and furniture hardware are all stamped in large numbers, which is the point. The family list is a starting filter, not an exhaustive taxonomy.
See metal stamping for the process behind these part families, custom stamping services for the service that runs them, and sheet metal fabrication for the low-volume route to the same geometry.
Scope and sources. The industry and part-family table — automotive brackets and heat shields at 100,000 to 2 million a year, electrical connectors and EMI shields at 500,000 to 50 million, medical and dental parts at 5,000 to 100,000, and robotics brackets at 1,000 to 50,000, together with the material notes for each family — comes from a review of industries that rely on stamped parts. The product-category breakdown covering enclosures and housings, brackets and mounts, electrical contacts and terminals, shims and spacers, chassis and frames, and springs, together with the four material groups and the standard tolerance band of plus or minus 0.005 to 0.015 inches, come from a buyer guide to stamped metal products. The industry to part and process map — body panels and chassis parts on transfer and progressive dies, connectors and shielding cans at plus or minus 0.05 mm, aerospace brackets in aluminium and titanium, and medical parts in stainless — comes from a classification of stamping parts and applications. This version replaces the unsourced production example and the industry statistics that appeared in an earlier version of this answer. Volumes, thicknesses and tolerances are planning ranges for a quotation discussion and not a standard; the number for a specific part comes from a die quote against a specific drawing.
Are you looking for a reliable manufacturer of down home textile products?
We can quickly provide customers with market analysis, technical support and customized services.From concept to product
From prototyping to production, our production sites can handle all your manufacturing projects.
subscription